1. Drop Forging Hall
Equipped with high-tonnage drop forging hammers and precision alloy dies, our forging division shapes raw high-grade stainless steel into dense, seamless blank forgings with enhanced structural integrity and grain alignment.
As a leading surgical instruments manufacturer in Pakistan, Rigor Instruments operates a fully modernized 30,000-square-foot integrated facility in Sialkot. Designed to fulfill the stringent requirements of international medical distributors, healthcare groups, and OEM brands, our manufacturing complex seamlessly combines administrative excellence with heavy precision engineering.
We firmly advocate complete in-house manufacturing. From raw steel selection (imported German and Japanese AISI 410, 420, and 316L surgical stainless steel) to die-forging, CNC machining, heat treatment, surface finishing, ultrasonic cleaning, and final autoclave sterilization testing, every single production stage is completed under one roof.
This zero-subcontracting framework ensures absolute batch consistency, full material traceability, and strict compliance with international medical device quality systems.
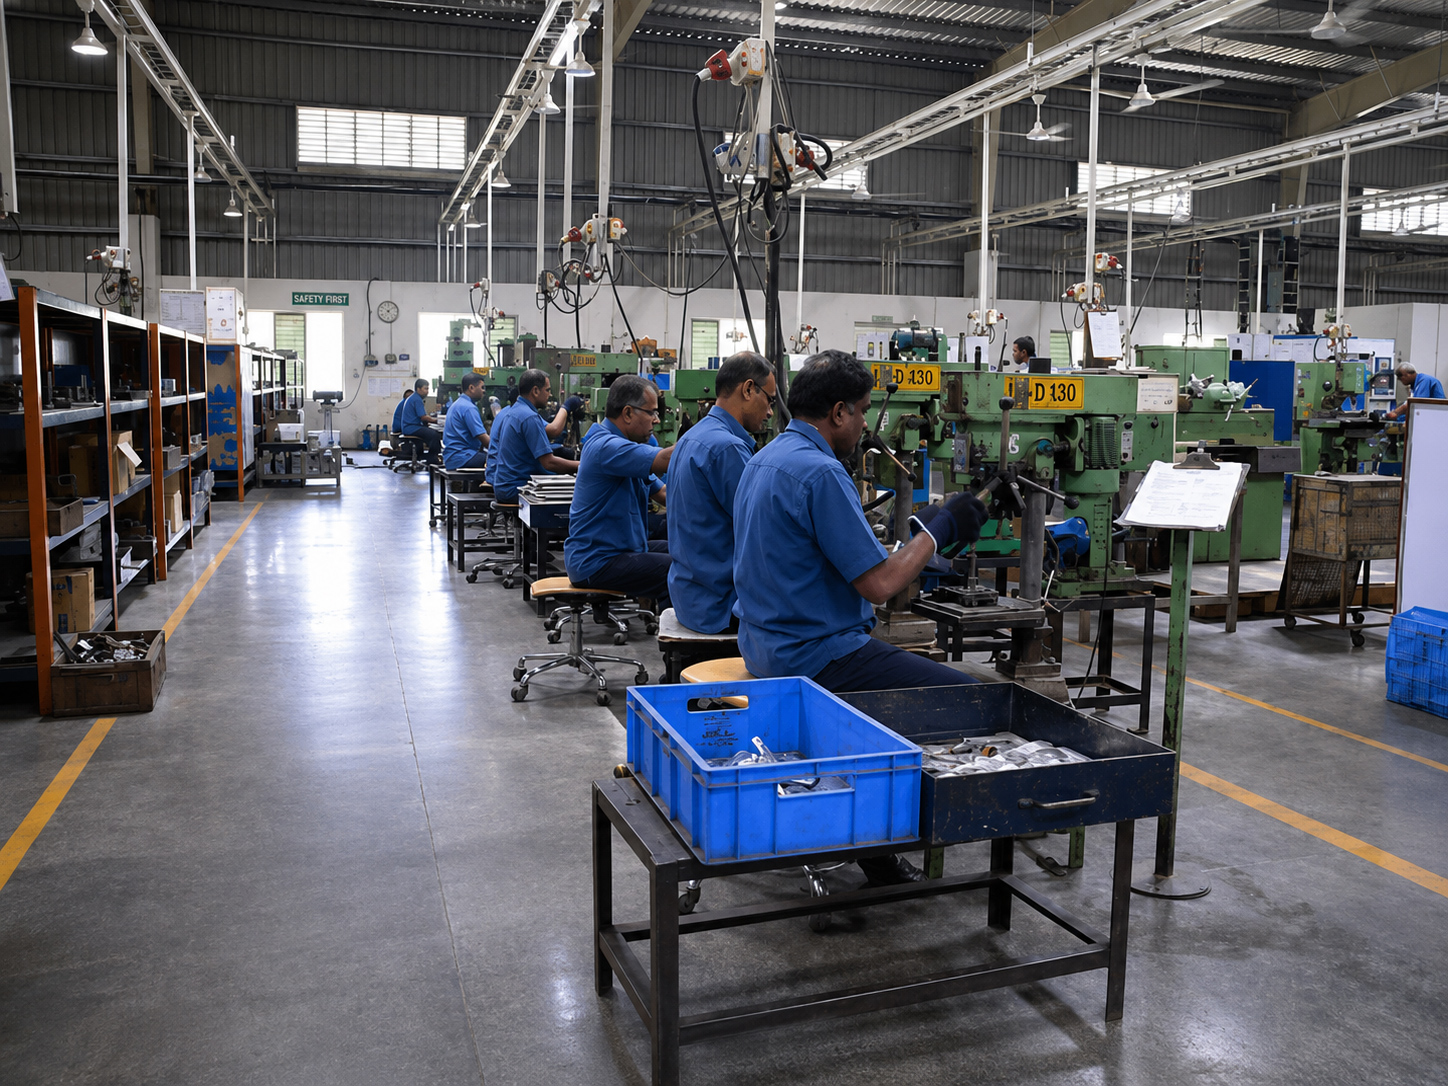
Our facility is structured into six dedicated technical divisions, each engineered to maintain sub-millimeter tolerances and flawless instrument craft.
Equipped with high-tonnage drop forging hammers and precision alloy dies, our forging division shapes raw high-grade stainless steel into dense, seamless blank forgings with enhanced structural integrity and grain alignment.
Utilizing multi-axis computer numerical control (CNC) milling and lathing machinery, this department crafts intricate surgical ratchets, box locks, delicate jaws, and micro-instruments to exacting CAD specifications.
Master artisans with decades of specialized craft perform rough and fine grinding. Blades, scissors, and forceps teeth are ground to micro-tolerances to achieve effortless cutting edges and anatomical alignment.
Featuring automated electro-polishing and cleanroom hand-buffing setups. Instruments receive anti-glare satin, mirror, or matte finishes to mitigate glare under operating room surgical lights.
Surgical instruments require human finesse. In our setting division, veteran technicians hand-adjust ratchet tension, jaw parallelism, and spring action to ensure effortless tactile control for surgeons.
A temperature-controlled environment where finished instruments undergo passivation testing, ultrasonic cleaning, laser etching of custom logos and serial numbers, and protective export packaging.
Our ISO 13485 medical device quality management system mandates stringent multi-point inspections throughout the manufacturing lifecycle.
Spectrometer analysis of incoming raw steel batches to verify chemical composition, corrosion resistance, and hardness compliance (HRC).
Optical comparators and digital calipers inspect milled joints, teeth alignment, and jaw dimensions after every machining stage.
Chemical passivation treatments followed by boiling and copper sulfate tests to guarantee zero rust formation during autoclave cycles.
100% manual inspection for smooth articulation, grip security, jaw closure, and sterile packaging before global container dispatch.
Whether you require wholesale bulk supplies, custom OEM manufacturing, or private-label packaging for medical instruments, our engineering team in Sialkot, Pakistan is ready to assist your organization.